A Membrane Bioreactor (MBR) combines biological treatment with membrane filtration in one process. Microorganisms in an aerated tank break down the organic load, and submerged or external membranes then separate the treated water from the sludge. This replaces the secondary clarifier and tertiary filters of a conventional plant.
Where MBR is the right choice
- Sites with very limited space, such as basements of commercial buildings
- Projects where treated water is to be reused for flushing, cooling or landscaping
- Upgrades where stricter discharge norms have to be met
- Pre-treatment for RO recycling and Zero Liquid Discharge schemes
System components
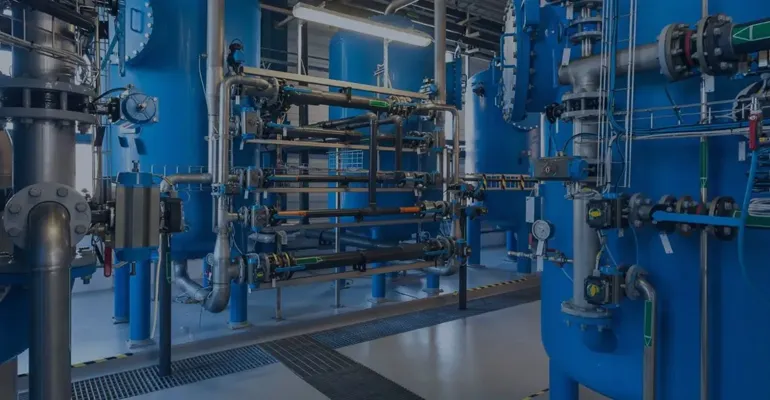
A typical MBR plant includes fine screening, an equalisation tank, an anoxic/aeration tank, membrane modules, permeate and backwash pumps, chemical cleaning (CIP) and an automated control panel.
Benefits
- Consistently clear treated water with very low suspended solids
- Smaller footprint than conventional activated-sludge plants
- Treated water suitable for further treatment by RO
- Automated operation with continuous monitoring
Abhay Enviro Engineering designs MBR plants on your flow rate and wastewater analysis, and provides commissioning, operator training and long-term O&M support.
